Thermal transfer ribbon slitting machine looks simple on paper: take a wide jumbo roll, cut it into narrow finished rolls, and ship them to printer users. In practice, the machine you choose determines whether your finished ribbons run smoothly through high-speed printers or become a source of complaints about broken ribbons, print misalignment, and damaged print heads. With ribbon substrates now as thin as 4.5 microns, selecting a slitter is not a matter of comparing price tags or maximum speed claims. It requires matching the machine to your material mix, precision requirements, and production volume.
This guide walks through the parameters that matter, the specifications that mislead, and the practical steps that separate a sound investment from an expensive lesson.
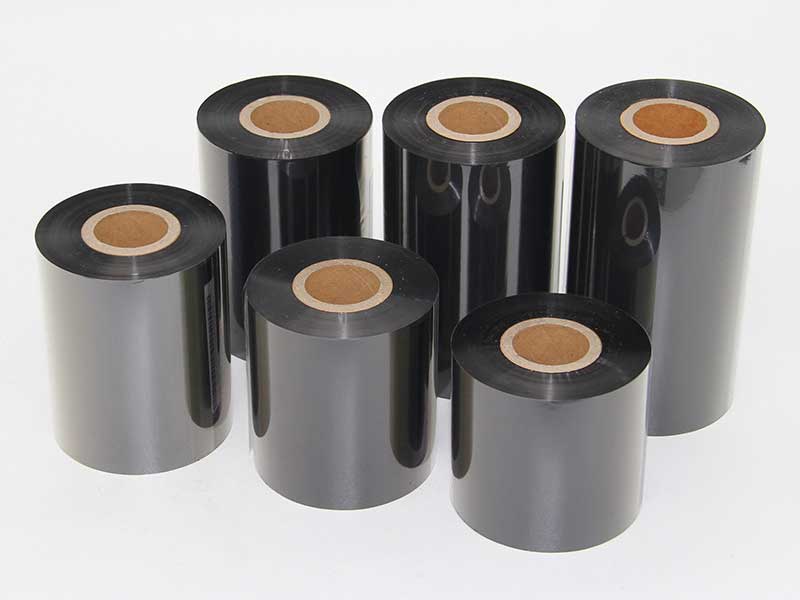
Start With Your Material, Not the Machine
The ribbon types you process most often should drive every specification decision. Wax-based ribbons are relatively soft and tolerate higher slitting speeds and more forgiving tension settings. Resin-based ribbons, with their harder coatings and lower toughness, typically require speeds 20–30% lower than wax ribbons and demand tighter tension control . Wax-resin hybrid ribbons fall between these extremes.
Thickness matters just as much. Standard thermal transfer ribbon films range from 4 to 20 microns, but substrates below 5 microns are especially sensitive to tension fluctuations. If your product mix includes ultra-thin specialty films alongside standard commercial ribbons, prioritize equipment with a wide, well-controlled tension range rather than a machine optimized for a single material type .
This material-first approach has a direct commercial consequence. A machine rated at 400 m/min may be perfectly capable of running your resin ribbon at 280 m/min. But if you primarily convert resin ribbons and pay a premium for a high-speed model you cannot fully utilize, that extra capital does not translate into proportional productivity .
Slitting Precision: The Quality Threshold
Slitting accuracy determines width consistency and edge quality. Both directly affect how the ribbon performs in the printer. Burrs or rough edges can damage print heads, while width deviations cause print displacement or ribbon misalignment during high-speed printing .
Industry accuracy tiers break down roughly as follows:
| Accuracy Grade | Tolerance Range | Typical Applications |
| Standard | ±0.3–0.5 mm | Commercial labels, logistics, warehousing |
| High Precision | ±0.1 mm | Electronics, pharmaceutical traceability, general industrial |
| Ultra-High Precision | ±0.05 mm or tighter | Medical labels, high-resolution barcodes, ultra-narrow ribbons under 10 mm |
When evaluating accuracy claims, ask the manufacturer to run a trial cut using your own ribbon master roll. Measure width deviation with a caliper across at least ten consecutive rolls, and inspect cut edges for burrs or coating delamination. Parameter tables reflect ideal laboratory conditions; your material reflects reality .
The hardware behind precision matters as much as the specification sheet. Key components include a tool shaft with radial runout under 0.01 mm, quality blades from established suppliers, and an edge position correction system. CCD vision correction suits transparent or semi-transparent materials, while ultrasonic sensors work better with opaque ribbons. Without a functional correction system, width tolerance is a theoretical number rather than a production reality .
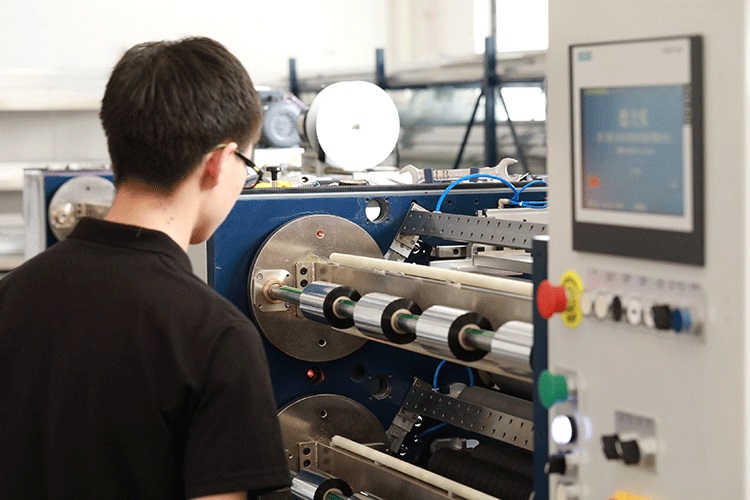
Tension Control: The Operational Core
Tension control is widely considered the single most important factor in ribbon slitting. The PET base film is extremely thin and behaves elastically under load. Excessive tension stretches and deforms the substrate, causing ink layer cracking and powder shedding that contaminates print heads. Insufficient tension produces loose, wrinkled rolls that generate white lines or indentations during printing. Uneven tension leads to telescoping or core misalignment .
For quality-focused production, prioritize a fully automatic closed-loop tension control system, typically combining a PLC with servo drives. This configuration monitors and adjusts tension in real time across unwinding, traction, and rewinding stages, holding fluctuations within ±2% of the set value. For thin substrates, look for systems that incorporate taper tension—tension that decreases dynamically as the rewinding diameter grows—to prevent internal creep and the “tight inside, loose outside” defect .
On the rewinding side, slip shafts are essential for multi-specification production. Each winding station has an independent slip ring that adjusts torque as roll diameter changes, maintaining consistent hardness from core to surface. Pneumatic slip shafts offer better control precision than mechanical versions and are worth the additional investment if you frequently switch specifications .
Slitting Speed: Match Output to Material Realities
Nominal maximum speed is the most heavily marketed specification and the least meaningful in isolation. What matters is the stable, repeatable speed your machine can sustain with your actual materials .
As a reference framework:
| Speed Class | Range | Best For |
| Low-speed economy | 50–100 m/min | Small batches, high-mix production |
| Medium-speed universal | 150–250 m/min | Most commercial orders |
| High-speed production | 300–500 m/min | Large-volume continuous production |
When a manufacturer quotes a top speed, ask under what material and tension conditions that speed was achieved. Then test with your own ribbon at that speed and evaluate start-stop control, winding neatness, and whether the machine maintains tension stability without operator intervention. A unit that claims 450 m/min but requires constant tension adjustments is less productive than a 250 m/min machine that runs unattended .
Automation Level and Changeover Efficiency
Automation directly impacts labor costs, changeover speed, and waste rates. The market offers three broad tiers. Semi-automatic machines require manual blade positioning and core loading, making them suitable for operations with limited product variety and lower labor costs. Fully automatic models handle blade setting, leader and trailer application, turret rewinding, and cross-cutting without operator intervention .
For factories facing frequent order changes and fragmented production runs, rapid changeover capability deserves serious attention. A control system with parameter memory can store complete slitting recipes for different ribbon widths and materials, enabling one-touch changeover. This reduces dependence on experienced operators and shortens downtime between batches . If your order book includes multiple narrow-width products, automatic blade setting can reduce setup time from minutes to seconds while eliminating manual positioning errors .
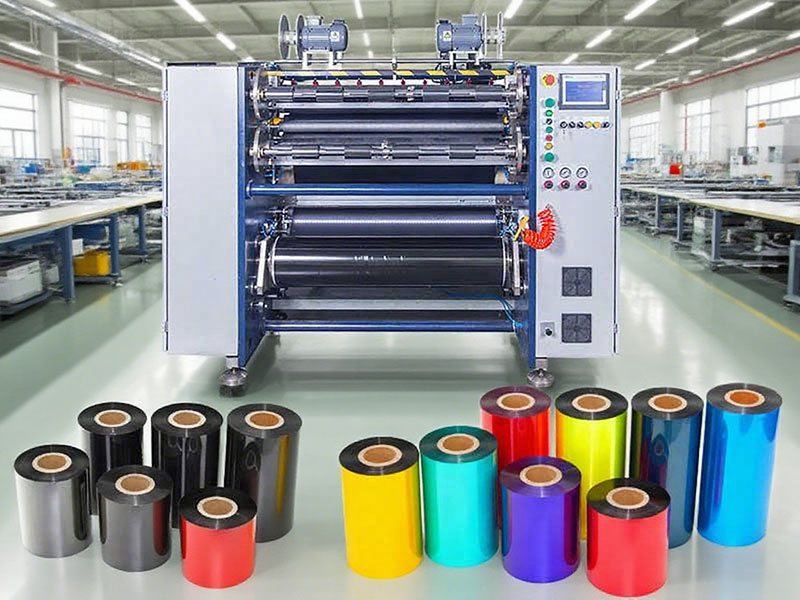
What the Specification Sheet Will Not Tell You
Several critical factors rarely appear in promotional materials but directly affect long-term satisfaction.
Frame rigidity determines whether a machine holds its accuracy after years of operation. Heavy, high-strength cast iron or steel frames absorb vibration and preserve alignment. The brands of drivetrain bearings, linear guides, and servo motors reflect the manufacturer’s commitment to durability .
Blade type and holder design should match your material. Square blades (razor type) suit ribbons below 70 microns and deliver higher precision and edge uniformity. Round blades (scissor type) handle thicker materials above 100 microns and paper-backed ribbons with greater durability. Magnetic clip holders allow quick width changes without tools, a practical advantage for multi-specification operations .
Waste edge handling affects material yield and housekeeping. A servo-driven waste rewinding unit maintains consistent tension on the trimmed edges, preventing tangles and reducing downtime .
Floor space and utilities are easy to overlook. Confirm the machine’s footprint against your available space, and verify power requirements (single-phase versus three-phase) and pneumatic supply specifications before installation .
The Trial Cut: Your Most Important Due Diligence
No specification sheet substitutes for a trial cut with your own material. Before committing to any purchase, insist on running your ribbon master roll through the machine under conditions that match your production environment.
Evaluate three things during the trial. First, measure width consistency across at least ten consecutive finished rolls using a caliper. Second, inspect the cut edges under magnification for burrs, coating delamination, or raggedness. Third, examine the wound rolls for end-face evenness—look for telescoping, “bell-mouth” deformation, or internal wrinkles that signal tension control problems .
If the manufacturer cannot accommodate a trial with your material, that itself is informative. A supplier confident in their equipment will welcome the test.
Matching the Machine to Your Business Model
The right slitting machine depends on where your factory sits in the value chain.
Small converters and print service providers with limited capital and varied but low-volume orders should prioritize a reliable medium-speed machine with solid tension control and quick changeover capability. Maximum speed is less important than consistent quality and minimal waste .
Specialty ribbon manufacturers producing narrow-width or resin-based products for electronics, medical, or high-resolution barcode applications need high-precision equipment with closed-loop tension control, taper tension, and correction systems. The investment in ±0.05 mm accuracy pays for itself through reduced customer complaints and print head damage claims .
High-volume ribbon converters serving commodity label markets should evaluate fully automatic production machines with turret rewinding and integrated leader/trailer handling. Labor cost savings and continuous operation justify the higher capital expenditure when volumes are sufficient .
The common thread across all three profiles is this: choose the machine that matches your actual production reality, not the one with the most impressive brochure. Your ribbon, your orders, and your operators will determine whether the investment delivers returns or becomes a source of downtime. Test before you buy, and let the trial cut make the final argument.
 English
 Deutsch
 Français
 Español
 Português
 日本語
 русский
 한국어
 عربي
 ภาษาไทย
 Tiếng Việt
 Italiano




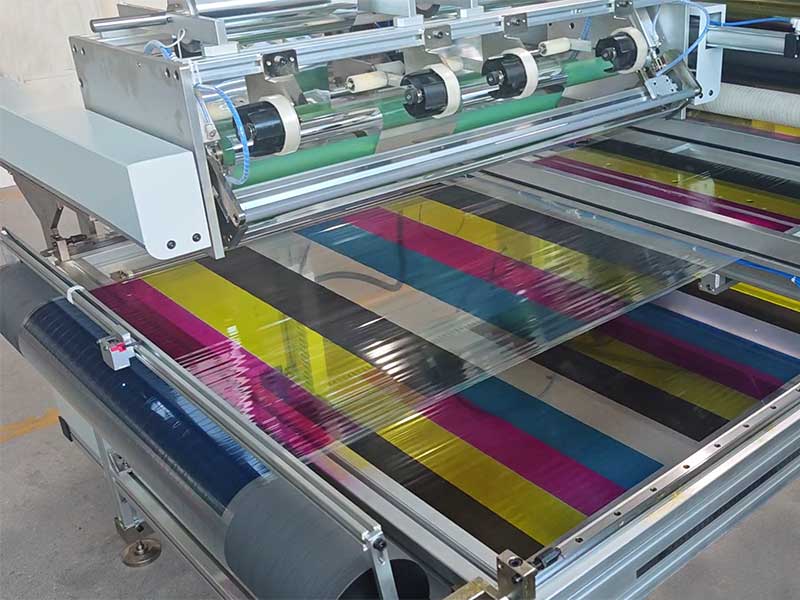
 Barcode Ribbon Slitting Machine
 Semi Automatic Thermal Transfer Ribbon Slitter RSDS5 PLUS
 Automatic Thermal Transfer Ribbon Slitter RSDS8 H PLUS
 Automatic Thermal Transfer Ribbon Slitter RSDS6 PLUS
 Solar Film Slitter
 Semi Automatic Thermal Transfer Ribbon Slitter RSDS1 PLUS
 Semi Automatic Thermal Transfer Ribbon Slitter RSDS2 PLUS
 Automatic Thermal Transfer Ribbon Slitter RSDS8 PLUS






