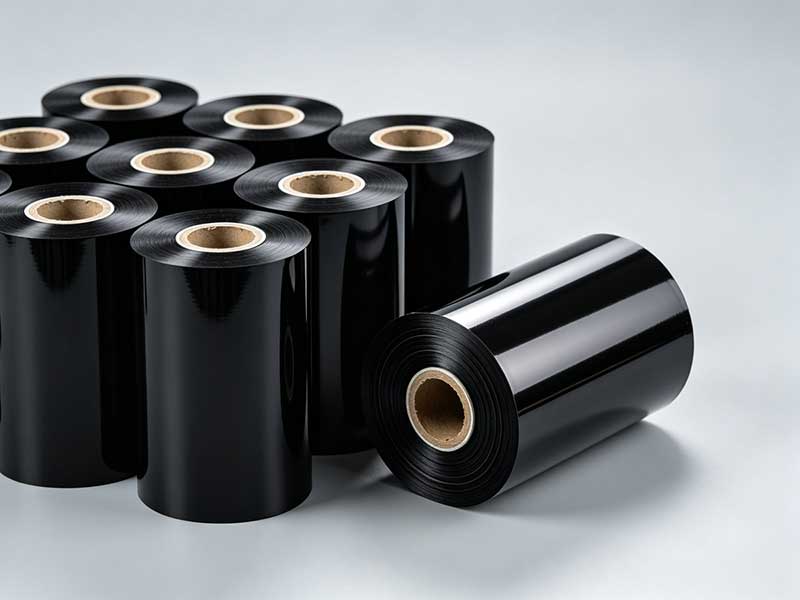
The total thickness of thermal transfer ribbons is usually only 4.5 to 20 microns, composed of an ultra-thin PET base film, heat-resistant coating, and ink layer. Slitting, as the final step before leaving the factory, directly determines whether the ribbon can be smoothly loaded onto the machine and whether the print head is damaged. When facing equipment on the market ranging from tens of thousands to hundreds of thousands of yuan, parameter lists are often densely packed, but what truly determines product quality and production efficiency are concentrated in a few key dimensions.
No need to be overwhelmed when choosing a model. By focusing on the three lifelines—slitting accuracy, tension control, and rewinding neatness—and rationally examining speed and hardware configuration, most pitfalls can be avoided.
1. Slitting Precision: The Lifeline of Quality
Slitting accuracy is the primary indicator for measuring equipment performance, directly determining the width consistency and edge quality of the finished ribbon. The cost of insufficient precision is real: rough ribbon edges, tape misalignment during printing, tape jams, and in severe cases, even wear the print head.
Industry precision standards can be roughly divided into three levels. Standard-grade accuracy is ±0.3~0.5mm, suitable for conventional commercial and logistics labels; The high-precision grade can reach ±0.1mm, meeting the needs of precision electronics and general industrial applications; The ultra-high precision level can be controlled within ±0.05mm, suitable for high-end scenarios such as medical labels and ultra-narrow ribbons. The key hardware determining accuracy lies in the rigidity of the tool holder and the stability of the transmission system. When purchasing, do not trust the theoretical values on the parameter table. Always bring your own ribbon master roll for on-site trial cutting, use a vernier caliper to measure the deviation between the slitting width and the set value, and check the sample edges for burrs or stringing.
2. Tension Control: The "Soul" of the Equipment
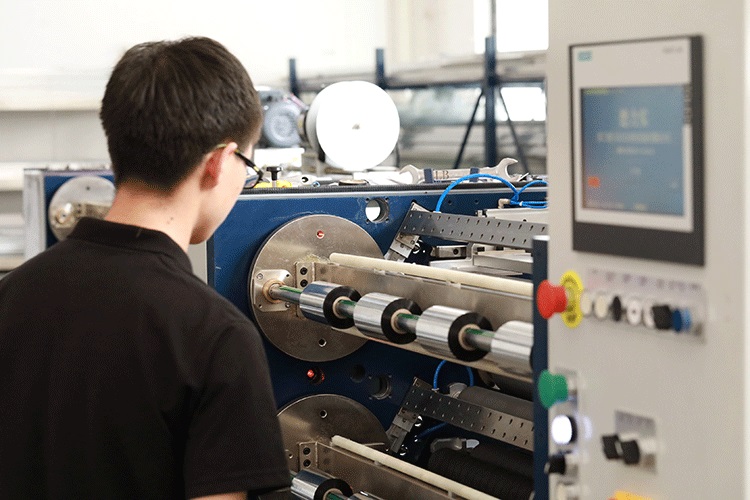
The PET base film of the ribbon is extremely thin and highly sensitive to changes in tension. Within the industry, tension control is regarded as the "soul" of slitting machines, with its impact on winding flatness accounting for over 50%.
Excessive tension results in the base film stretching and deformation, causing microcracks in the ink layer, which leads to powder loss and white lines during printing; If the tension is too low, the ribbon becomes loose and wrinkled, and the winding end face becomes "snake-shaped," making core misalignment during transportation more likely. Excellent tension control schemes adopt differentiated zones: the unwinding area uses decreasing tension, the slitting area maintains constant tension, and the winding area implements tapered decreasing control—reducing tension linearly as the coil diameter increases, preventing the outer layer from overtightening and crushing the inner layer, forming a "daisy core" winding.
When purchasing, priority should be given to fully automatic closed-loop tension control systems. It uses real-time feedback from tension sensors and dynamic adjustment by PID algorithms to control fluctuations within an extremely narrow range. Traditional open-loop control (such as manually adjusting the magnetic powder clutch) struggles to handle tension drift caused by changes in coil diameter, especially during high-speed start-stop.
3. Uniformity of Wrapping: The Overlooked "Hidden Costs"
The neatness of winding directly affects the efficiency of post-process packaging and the smoothness of the printer's belt movement. The end face is "bell-mouthed," edges are "serrated," or internal wrinkles are all caused by inadequate tension control and correction devices. These issues can easily cause ribbon breakage or cartridge breakage during subsequent rewinding printing.
Industry control standards are: face deviation should generally be controlled within ±1mm, and for high-end equipment, it can reach ±0.5mm. To reach this level, besides closed-loop tension control, slip shafts are essential for high-end ribbon production. It can independently control the torque of each winding unit and adjust in real time according to changes in coil diameter, effectively solving the issues of "loose inside" or "tight outside" or "vegetable core" when winding multiple rolls simultaneously. Pneumatic slip shafts offer higher control accuracy than mechanical ones, making them especially suitable for production scenarios requiring frequent specification changes. Additionally, active deviation correction systems are indispensable; CCD photoelectric or ultrasonic sensors can detect the ribbon edge position in real time and automatically adjust the path to prevent minor misalignment during high-speed operation.
4. Slitting speed: The measure of efficiency, but higher is not always better
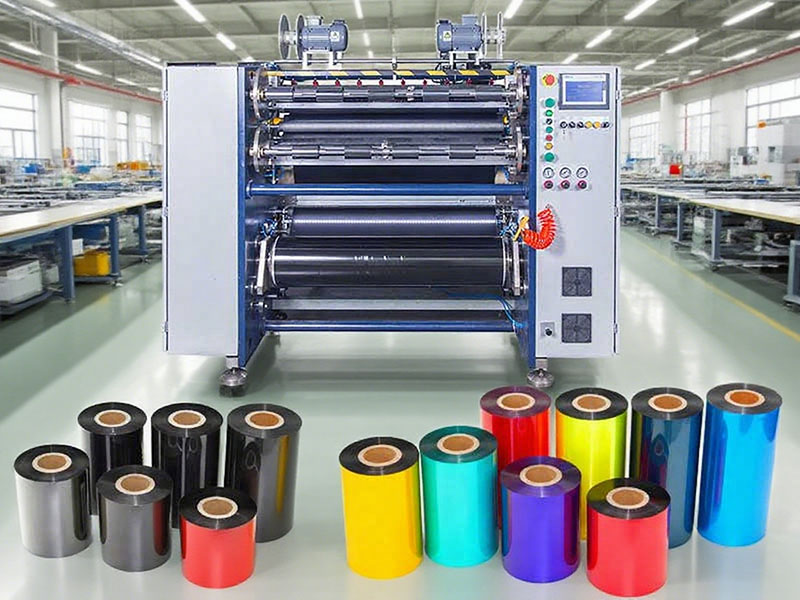
Slitting speed determines output per unit time, but the nominal maximum speed is often just "lab data." A device that frequently slows down or stops due to tension fluctuations may actually produce less output than a stable medium-speed model.
Speed ratings can refer to the following ranges: low-speed economical type 50~100 m/min, suitable for small batches and multi-variety production; Medium-speed universal model 150~250 m/min, meeting most commercial orders; High-speed production model 300~500 m/min, suitable for large-scale continuous production. It is important to note that the actual usable speed is significantly affected by the ribbon material. Resin-based ribbons have harder coatings and lower toughness, so they usually need to operate at speeds 20%~30% lower than wax-based ribbons. Therefore, when evaluating speed, manufacturers should be asked to test cut using your actual materials and observe the rewinding state during high-speed start and emergency stop, rather than just looking at the highest speed when empty.
5. Hardware and long-term costs that are often overlooked
Beyond the parameters, the hardware configuration of the device determines the long-term user experience. Frame rigidity is worth noting: thick cast iron or steel frames can effectively absorb vibrations during slitting, ensuring accuracy retention after years of high-speed operation. In terms of tool systems, circular blades are suitable for high-speed slitting, while flat (square) blades have neater cuts and less dust for thin ribbons. The lifespan of cemented carbide or ceramic-coated inserts is significantly better than that of ordinary high-speed steel. The reel specifications must match your finished core—1-inch and half-inch are common configurations; confirm the device is compatible with your current and future specifications.
Finally, after-sales service and trial testing verification are the most important "insurance" in product selection. Ribbon slitting machines involve precise tension and correction debugging, and the supplier's response speed and technical support capabilities directly affect downtime losses. Before making a final decision, it is recommended to bring your own master roll to visit at least three suppliers, compare slitting effects with the same roll material, and measure width tolerances, end face deviations, and edge quality. A device with attractive parameters but burrs on the edges of the sample is not worth the risk.
 English
 Deutsch
 Français
 Español
 Português
 日本語
 русский
 한국어
 عربي
 ภาษาไทย
 Tiếng Việt
 Italiano





 Ribbon Slitting Machine
 Barcode Ribbon Slitting Machine
 Semi Automatic Thermal Transfer Ribbon Slitter RSDS5 PLUS
 Automatic Thermal Transfer Ribbon Slitter RSDS8 H PLUS
 Automatic Thermal Transfer Ribbon Slitter RSDS6 PLUS
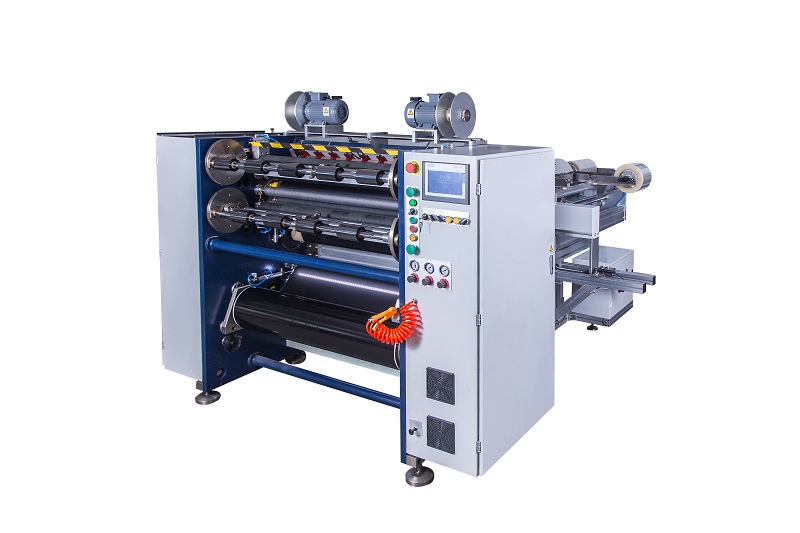 Semi Automatic Thermal Transfer Ribbon Slitter RSDS2 PLUS
 Card Print Ribbon Rewinder
 Semi Automatic Thermal Transfer Ribbon Slitter RSDS1 PLUS






