In the hot stamping industry, there is an old saying: “Thirty percent stamping, seventy percent slitting.” The quality of your slitting process directly determines whether your foil performs as intended in the stamping press, and ultimately, whether your customer accepts the finished job. A slitter that matches your material profile and production rhythm transforms wide master rolls into flawless finished strips. The wrong one generates burrs, scratches, and constant downtime—wasting expensive foil and eroding your margins.
This guide breaks down the selection process into the dimensions that actually matter for buyers who cannot afford to guess.

Start With Your Material, Not the Spec Sheet
Hot stamping foil is not a single product. Its structure—typically a PET base film carrying release, color, and adhesive layers—makes it far more sensitive to handling than paper or standard films. The specific foil type you process most often should dictate your equipment priorities.
Standard colored foil is the most forgiving. It has moderate resistance to tension variation and works well with standard-precision equipment using circular blade slitting and basic static elimination.
Laser and holographic foils present the greatest challenge. Their surface carries a fine diffraction microstructure that is easily scratched by any contact. For these materials, air knife (non-contact) slitting becomes almost essential, and every guide roller in the material path should be mirror-polished to prevent microscopic abrasion.
Thin gauge foil (12–19μm) demands superior tension control. The base film stretches permanently if tension runs even slightly high, causing registration errors downstream. If tension runs low, air gets trapped between wound layers, leading to telescoping and interlayer slippage.
Adhesive-heavy foils tend to gum up cutting edges. Teflon-coated blades and mirror-finish rollers help prevent sticking, while a carefully tuned micro-tension system avoids the stretching that activates the adhesive prematurely.
Before comparing machine models, document your actual material profile: typical thickness range, base film type, surface sensitivity, and the narrowest width you need to produce. Bring this to every supplier demonstration.

Cutting Method: The Choice That Determines Edge Quality
The cutting mechanism directly controls burr formation, dust generation, and blade longevity. Three main approaches exist, each suited to different production profiles.
Shear cutting (circular blades) remains the mainstream choice for hot stamping foil. Upper and lower disc blades act like scissors, producing clean edges with minimal dust. Blade life is relatively long, and the method handles a wide range of thicknesses. The trade-off is higher mechanical complexity—cutter shaft rigidity becomes critical, especially for widths above 800mm where mid-shaft deflection can cause incomplete cuts.
Razor blade slitting is the economical option. It suits narrow-width applications and lower-volume production. However, razor blades generate more dust and burrs on thicker foils, and blade replacement is frequent. For factories producing standard packaging foil in modest volumes, it remains a viable cost-conscious choice.
Air knife (non-contact) slitting uses high-pressure air to separate the material. It eliminates blade-induced scratches entirely, making it the only safe option for laser and holographic foils with delicate surface structures. The drawbacks are higher initial cost and suitability primarily for thinner gauges.
For factories running a mix of standard and specialty foils, a shear-cut machine with quick-change blade assemblies offers the best balance of versatility and edge quality.
Tension Control: The Invisible Factor That Makes or Breaks Quality
If one technical specification separates adequate slitters from excellent ones, it is tension control. Hot stamping foil is unforgiving—slight tension errors cause stretching, wrinkling, or telescoping that only become apparent downstream at the hot stamping press.
Open-loop tension control relies on preset values and magnetic particle brakes. It is acceptable for low-speed, non-critical applications below roughly 100 m/min, but it cannot compensate for diameter changes during winding or for acceleration/deceleration disturbances.
Closed-loop servo tension control uses tension sensors or floating dancer rollers to measure actual tension in real time and adjust the unwinding and rewinding drives accordingly. For hot stamping foil, this is the minimum acceptable specification. A quality closed-loop system maintains tension fluctuation within ±1% to ±3% of the set value. For 12μm ultra-thin PET, this level of control is not a luxury—it is the difference between sellable foil and scrap.
Taper tension is equally important on the winding end. As the finished roll grows in diameter, winding tension must decrease according to a set curve. Without taper tension, the inner layers get crushed, causing “chrysanthemum core” defects or interlayer slippage during narrow slitting. For hot stamping foil, a taper coefficient between 60% and 80% is recommended, with final tension reduced to 40–70% of the initial value.
When evaluating machines, ask for tension control accuracy specifications and request a demonstration using your thinnest, most tension-sensitive material.

Width Capacity and Narrow-Slit Precision
The width specification of a slitting machine has two dimensions: the maximum unwind width and the minimum slit width. Both must align with your production reality.
For wide-format operations processing master rolls up to 1600mm or 2000mm, the critical specification is frame rigidity and blade shaft diameter. Wider slitting means greater cantilever forces on the blade shaft; if the shaft flexes even slightly under pressure, the center of the web will not cut through while the edges are over-penetrated. Look for machines with thickened alloy steel wall panels and large-diameter, dynamically balanced blade shafts.
For narrow-strip production below 50mm—common for hot stamping lines serving cigarette packs, liquor labels, and security applications—the priorities shift to tool positioning precision and anti-winding design. Manual locking systems are prone to dimensional drift because uneven clamping forces allow axial movement during operation. Hydraulic locking or high-precision slip shafts are the more reliable choice when slit widths are measured in millimeters. If your order profile includes frequent width changes, an automatic tool positioning system can reduce changeover time from hours to minutes.
A practical benchmark: if your master roll is 640mm and your finished rolls are 20mm wide, the machine must be capable of holding ±0.5mm tolerance at that narrow width.
Web Guiding: The Often-Overlooked Stability Factor
The edge guiding system ensures that the foil maintains correct lateral alignment throughout the slitting process. Misalignment results in uneven end faces, telescoping, and downstream feeding problems at the stamping press.
For hot stamping foil—especially holographic and metallized varieties—ultrasonic sensors are strongly preferred over photoelectric sensors. Photoelectric detection can be unreliable with reflective or metallic materials, whereas ultrasonic detection is unaffected by color, transparency, or surface reflectivity. Also inquire about the response speed of the correction actuator; it must be capable of millisecond-level adjustments during high-speed operation.
Automation Level: Matching Machine Intelligence to Your Order Profile
The economics of hot stamping foil production increasingly favor flexibility over raw speed. Order specifications have surged from a few traditional types to dozens of varieties, while single batch sizes have plummeted. If a single equipment change requires more than half an hour of downtime, small batch orders simply cannot generate profit.
Key automation features to evaluate include automatic tool positioning for rapid width changes, servo-driven rewinding with independent tension control for each finished roll, and programmable recipe storage for recurring order profiles. A machine with programmable control can eliminate manual adjustments, saving up to 30% in setup time compared to non-programmable alternatives.
That said, do not pay for automation you will not use. A converter running long production runs of the same few widths may find manual positioning perfectly adequate, while a job-shop serving diverse packaging customers will quickly recoup the investment in quick-change systems.
Speed: Match Capacity, Not Marketing Numbers
The nominal speed of hot stamping foil slitting machines is commonly quoted as 200–600 m/min. However, the labeled “maximum speed” is the limit value under ideal conditions; the actual stable operating speed is the reference point. High-speed operation demands tension control, correction accuracy, and rack rigidity that increase exponentially with speed. Blindly chasing higher speed may result in frequent downtime and debugging and a large amount of scrap.
Ask the supplier to demonstrate the machine running your material at the speed you actually intend to operate. Observe edge quality and dimensional consistency across a continuous run of at least one hour, not just during the initial startup phase. A machine that performs well on ideal materials may struggle with the specific coatings and substrates you use daily.
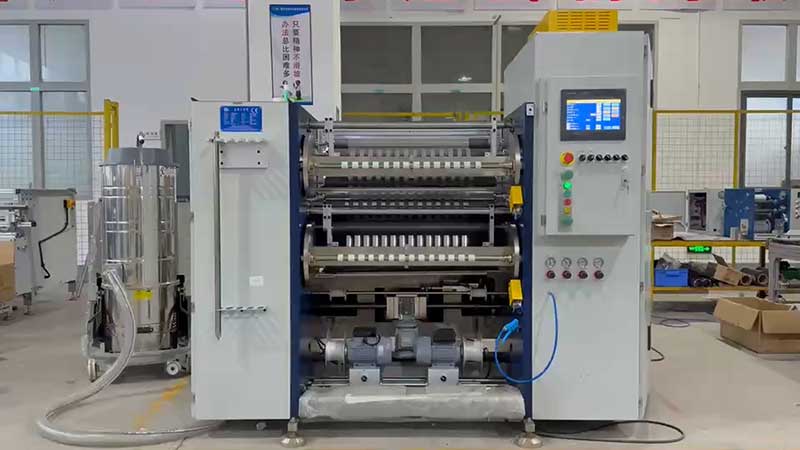
Questions to Ask Every Supplier Before You Commit
The market offers a wide range of machines with varying capabilities and price points. To avoid costly mistakes, bring a structured list of questions to every supplier conversation:
On accuracy: “Can you demonstrate dynamic slitting accuracy at full production speed using our foil samples?” Distinguish between static accuracy on a spec sheet and real-world performance under tension and speed.
On tension control: “Is the system fully closed-loop, and does it include taper tension functionality?” Request the tension fluctuation specification and confirm independent control for unwind, slit, and rewind zones.
On blades: “What blade material and coating are used, and what is the expected blade life with our adhesive formulation?” Diamond-coated or carbide blades offer significantly longer service life and more consistent cuts than standard steel. Also ask about blade engagement range—for hot stamping foil, this is typically 0.02–0.05mm with precise adjustment capability.
On winding neatness: “What is the specified end face alignment tolerance?” A high-quality machine should achieve end face misalignment of 0.1mm or less. Ask whether the rewinding shafts are air shafts, slip friction shafts, or both, and whether each finished roll can slip independently to compensate for slight thickness variations.
On support: “What is the spare parts lead time, and do you provide installation and training in our region?” A machine is only as good as the support behind it. Confirm warranty terms, local service availability, and whether consumables and wear parts are stocked regionally.
The Bottom Line
Choosing a hot stamping foil slitter is not about finding the machine with the highest top speed or the most impressive brochure. It is about matching the equipment’s capabilities to your specific material, your order profile, and your downstream quality requirements. A machine that performs flawlessly on standard 25μm foil may struggle with 12μm laser film. A unit optimized for 1600mm wide-format master rolls may not deliver the precision needed for 10mm narrow-strip production.
Start with your material. Define your narrowest width and your most tension-sensitive foil. Demand a live demonstration with your own samples. And remember that in hot stamping, the slitter is not a peripheral piece of equipment—it is where the quality of your finished job begins.
 English
 Deutsch
 Français
 Español
 Português
 日本語
 русский
 한국어
 عربي
 ภาษาไทย
 Tiếng Việt
 Italiano



 Cold Foil Slitter
 Card Print Ribbon Rewinder
 Card Print Ribbon Slitter
 Hot Stamping Foil Slitting Machine
 Holographic Foil Slitter
 Digital Enhancement Foil Slitter
 Hot Stamping Foil Slitter RSDS7H 1350 PLUS
 Hot Stamping Foil Slitter (RSDS7H) 1350






